Skip to content

Factory integration changes where AI infrastructure gets assembled, tested, and validated, but it does not remove the engineering obligations waiting at the destination. A factory-integrated pod can arrive with its internal systems connected and tested, yet its operating environment still depends on electrical interfaces, cooling capacity, structural support, network connectivity, and carefully controlled installation conditions. The building, access route, equipment foundations, and utility connections must support the complete system rather than simply accommodate its outer dimensions. That requirement changes how operators should assess a site before committing to delivery schedules or equipment procurement. Readiness becomes an engineering status that teams must demonstrate through documented inspections, interface checks, and acceptance tests.
The commercial appeal of DSX POD rests on moving substantial integration work away from the construction site and into a controlled manufacturing environment. Factory teams can complete internal cabling, piping, equipment installation, and functional validation before shipment, reducing the amount of work that remains at the destination. However, the final connections still depend on the condition and capacity of the receiving site’s infrastructure, including its electrical supply, heat-rejection systems, and networking interfaces. A completed pod cannot compensate for an undersized distribution system, an uncommissioned cooling loop, or a fiber route that terminates at the wrong location. These dependencies matter because an installation can appear physically complete while remaining unable to operate as an integrated computing system. The central engineering challenge is to certify the interfaces between the factory-validated product and the site that must support it, rather than treating delivery as proof of operational readiness.
Defining the Prepared Site Standard
A prepared site needs a more demanding definition than cleared ground, completed construction, or the availability of a utility connection. It must provide a verified physical and technical envelope within which the intended pod can be transported, positioned, connected, commissioned, and maintained. Civil readiness establishes whether access roads, drainage, foundations, equipment pads, and underground services can support the planned installation without unplanned reconstruction. Structural readiness confirms that the supporting surfaces and load-bearing elements can accommodate the actual equipment configuration, including concentrated loads and the forces introduced during lifting and placement. Electrical readiness requires evidence that the incoming supply, distribution equipment, protection arrangements, grounding, and connection interfaces match the approved deployment design. Cooling readiness must establish that the site’s fluid systems and heat-rejection equipment can deliver the required operating conditions across the intended load range, while network readiness confirms that external connectivity reaches the correct termination points.
The certified envelope should originate in the actual deployment configuration, not in a generic checklist applied identically to every site. Engineering teams first identify the selected pod configuration, its shipping dimensions, installed equipment, connection points, service clearances, operating environment, and anticipated maintenance procedures. They then translate those details into site-specific acceptance criteria that cover civil works, structural capacity, electrical interfaces, cooling performance, fiber routing, security, and emergency access. The resulting documentation should separate manufacturer-published requirements from project-specific engineering criteria, applicable code obligations, and assumptions that still require verification before the team approves the site for delivery. Recording these categories separately helps prevent preliminary design assumptions from becoming unverified acceptance criteria during construction and commissioning. It also gives procurement, construction, commissioning, and operations teams a common record against which they can verify completed work and resolve discrepancies before shipment.
Factory Validation and Site Acceptance Are Separate Gates
Factory validation establishes that the assembled equipment meets its defined internal configuration and test requirements before it leaves the manufacturing environment. That work can verify installed components, internal wiring, rack connectivity, fluid connections, controls, and other functions included in the manufacturer’s acceptance procedure. Site acceptance addresses a different set of conditions because the receiving environment introduces external electrical, hydraulic, mechanical, environmental, and communications dependencies that factory tests cannot independently prove. The distinction matters during commissioning because a successful factory test does not establish that the site’s electrical protection coordinates correctly with the delivered system or that the cooling plant can maintain its required operating conditions. Site teams must verify the external interfaces, check the completed connections, and test the integrated arrangement under an approved commissioning plan. The process should also preserve traceability between the factory test record, the shipped configuration, the as-installed condition, and the results of site acceptance testing.
A project-specific site acceptance record should identify the responsible engineer for each interface, the evidence required for approval, the procedure for resolving failures, and the authority responsible for releasing the site for delivery. Civil contractors can document foundation completion and surveyed dimensions, while structural engineers verify the applicable loading assumptions and supporting calculations. Electrical teams can record equipment ratings, protection settings, grounding arrangements, test results, and the status of the final connection points. Cooling specialists can document flushing, pressure testing, flow verification, fluid compatibility, control integration, and heat-rejection performance against the approved design. Network teams can certify route diversity, termination locations, optical testing, and connectivity to the intended network handoff, while the commissioning lead reconciles these records into one controlled acceptance package. The project team should authorize delivery only after the required evidence meets the approved project criteria and any unresolved deviations have documented corrective actions and assigned owners.
Transport Envelope and Rigging Readiness
A factory-integrated pod can meet its manufacturing specifications and still encounter a delivery constraint that prevents it from reaching its intended position. Transport readiness begins with the complete route, from the dispatch point to the final installation area, rather than with the entrance to the site alone. Road geometry, bridge restrictions, overhead clearances, turning movements, surface conditions, and temporary construction obstacles all affect the delivery plan. The shipping configuration also matters because transport dimensions, axle loads, center of gravity, and lifting provisions may differ from the assumptions used during preliminary site planning. Engineering teams must reconcile the shipping documentation with the route survey and confirm that the proposed transport arrangement can safely accommodate the actual load. A route that appears adequate for ordinary construction vehicles may still prevent a specialized transport vehicle from negotiating a restricted turn or reaching a suitable unloading position.
The Delivery Route Is Part of the Engineering Design
Route approval should therefore rely on documented measurements and verified vehicle requirements instead of visual inspection or general assurances from a logistics contractor. The survey should identify road widths, vertical clearances, turning radii, gradients, surface transitions, bridge restrictions, and any overhead utilities that could interfere with the planned movement. Teams should also establish whether the transport vehicle can reverse, turn, or reposition safely without crossing unverified ground or obstructing critical access routes. Temporary roadworks, construction fencing, parked equipment, and recently installed utility infrastructure can alter the route between the initial survey and the scheduled delivery. A controlled route plan should record these constraints, identify the parties responsible for removing them, and specify the conditions that would trigger another inspection. Where local road authorities require permits or escort arrangements, the delivery schedule must account for those approvals rather than treating them as administrative details.
The final approach deserves particular attention because it often combines the most restrictive geometry with the least forgiving ground conditions. A transport vehicle may negotiate public roads successfully yet struggle to cross a site entrance, temporary access road, underground service corridor, or recently backfilled trench. Construction teams should compare the vehicle’s actual wheel and axle loading with the verified capacity of the route, including temporary surfaces and structures that may not have been designed for heavy delivery traffic. Drainage channels, utility covers, culverts, and buried services require explicit review wherever vehicle loads could exceed their design assumptions. The route assessment should also identify safe stopping locations, turning areas, reversing arrangements, and the space needed to position the load for lifting. Weather conditions can change traction and bearing capacity, particularly on unfinished access roads or surfaces that rely on temporary stabilization.
Crane Pads, Staging Areas, and the Lift Plan
A suitable delivery route does not establish that the site can safely receive and position a factory-integrated pod. The lifting operation introduces a separate set of loads, clearances, ground conditions, and coordination requirements that must match the selected crane and lifting configuration. Crane selection depends on the load’s verified shipping weight, lifting radius, required hook height, boom configuration, rigging arrangement, and the obstacles between the crane and the final position. The crane pad must support the calculated ground pressures and the reactions transmitted through the crane’s outriggers or tracks under the planned lift. Engineers should review underground utilities, buried structures, retaining walls, slopes, drainage features, and adjacent excavations before approving the crane position. A surface that supports ordinary construction traffic may not safely support a crane operating near its planned lifting limits.
The staging yard must accommodate more than the delivered unit’s footprint because the unloading sequence depends on access for transport vehicles, lifting equipment, rigging personnel, and supporting machinery. The plan should define where each vehicle waits, how the load transfers between transport and lifting arrangements, and which areas must remain clear throughout the operation. Ground bearing capacity should be checked across the entire working area, including locations where vehicles may turn, stabilize, or temporarily carry concentrated loads. Teams must also account for overhead obstructions, crane tail swing, suspended-load travel, exclusion zones, and the possibility that the lift requires a different position from the one shown in early construction drawings. The receiving area should provide enough space for safe rigging access without forcing personnel to work between the load and fixed structures.
Structural Tolerance and Floor Loading Reality
Structural readiness requires engineers to evaluate how the complete pod transfers its weight into the supporting structure, rather than relying on a general floor-loading rating. The assessment must use the actual equipment configuration, including rack assemblies, power distribution components, cooling equipment, containment structures, and any ancillary systems included in the installation. Distributed loads and concentrated loads create different demands, particularly where heavy equipment rests on discrete support points rather than continuous foundations. Engineers must trace those forces through floor slabs, beams, columns, transfer structures, and foundations to establish whether the complete load path meets the approved design. The assessment should also consider installation loads because lifting equipment, temporary supports, and positioning operations can introduce forces that differ from normal operating conditions.
Load Paths Matter More Than Nominal Floor Capacity
Floor-loading calculations should reflect the difference between a published slab capacity and the actual reactions produced by the equipment’s support arrangement. A general rating expressed across a floor area cannot, by itself, demonstrate that a particular slab can safely support concentrated reactions near a joint, opening, column, or service trench. Engineers need reliable information about slab thickness, reinforcement, material properties, support conditions, embedded services, and the condition of the existing structure. Where drawings do not adequately describe the as-built structure, targeted investigation may be necessary before the design team can confirm the proposed loading arrangement. Equipment supports may require adjustment to distribute forces across a wider area, while some installations may need local strengthening or a revised equipment layout. Those decisions must follow structural calculations and approved design details rather than assumptions based on the performance of similar sites.
The support arrangement must also accommodate the forces associated with seismic restraint, equipment movement, and other actions specified by the applicable structural design. Heavy rack assemblies can create localized demands that differ from those of conventional computing equipment, especially when power and cooling components occupy the same support zone. Engineers should verify that anchors, restraints, base frames, and connection details transfer the required forces into the supporting structure without creating unapproved stress concentrations. Floor penetrations and service openings require coordinated review because they can interrupt reinforcement or reduce the effective capacity of the surrounding slab. The installation plan should identify the approved bearing locations and prevent contractors from relocating supports to simplify cable routing or piping connections. Any proposed change to the support geometry should return to the structural engineer for review before the team proceeds.
Flatness, Vibration, and Settlement Define Installation Quality
Structural capacity addresses whether the floor can carry the load, while surface tolerance determines whether the equipment can sit correctly on that floor. A slab may possess adequate strength yet contain unevenness that complicates alignment, distorts support contact, or places unintended forces on the equipment frame. The installation specification should define the required flatness, levelness, and elevation tolerances for the actual pod configuration and its mounting arrangement. Surveyors should measure the receiving surface against a controlled datum before delivery, then compare the recorded condition with the approved installation drawings. Where the surface falls outside the permitted envelope, the project team should correct it using an approved method that preserves the designed support conditions. Shimming, grouting, or other adjustment techniques should follow the equipment and structural requirements rather than compensate informally for an unsuitable foundation.
Vibration requires its own assessment because the source, frequency, and transmission path can matter as much as the overall movement measured at the floor. Nearby rotating equipment, generators, pumps, traffic, construction activity, and mechanical plant can transmit vibration through the building structure or through connected services. Engineers should determine whether the computing equipment, optical connections, cooling assemblies, or other sensitive components impose specific vibration limits under the approved installation conditions. Isolation systems may help control transmission, but their selection must account for equipment weight, dynamic behavior, support stiffness, and the movement introduced by connected piping or cabling. Flexible connections should accommodate the intended movement without creating unacceptable mechanical stress or compromising service integrity. Teams should evaluate vibration sources during both normal operation and foreseeable transitions, including the starting or stopping of large mechanical equipment.
Fiber Plant and Inter-Pod Fabric Preconditions
A factory-integrated computing system can reach its installation position with its internal connections intact and still remain unable to communicate with the wider computing environment. The external fiber plant determines whether the pod can connect to upstream networks, storage systems, management infrastructure, and other computing resources required by the deployment. Network readiness therefore depends on more than the presence of fiber cables somewhere within the site. Engineers must establish the required routes, termination locations, optical characteristics, connection interfaces, and physical separation between paths before the installation reaches its final stage. The network design must also account for the relationship between internal pod connectivity and the external fabric that links separate pods into a larger computing environment.
Network Readiness Begins Before the Pod Arrives
The first task is to map every external connection from the pod’s designated handoff point to its intended destination. That map should identify the fiber type, connector specification, termination panel, routing path, patching arrangement, and ownership of each connection. Network engineers must confirm that the physical plant supports the required optical characteristics and that the proposed equipment interfaces match the approved design. A cable that reaches the correct room does not necessarily provide a usable connection if the termination, polarity, connector type, or optical budget fails the system requirements. The route should also preserve access for inspection, testing, replacement, and future changes without requiring technicians to disturb unrelated services. Where several pods share a network spine, the design must specify how each pod connects to the spine and how the spine connects to the wider fabric.
Route diversity requires equal attention because two apparently separate fiber connections may still share a physical point of failure. Independent routes should be assessed across the complete path, including duct banks, building entrances, intermediate distribution spaces, risers, and final termination areas. Separate cables do not provide meaningful physical diversity if both pass through the same vulnerable duct, access chamber, or congested entry point. Engineers should document shared infrastructure and determine whether it meets the availability objectives established for the deployment. Diverse routing may require additional duct capacity, separate entry points, coordinated rights of access, or changes to the location of network equipment. The design should also protect fiber paths from crushing, excessive bending, water ingress, construction damage, and interference from other building services. A route-diversity review completed before civil works close out can prevent expensive changes after the pod has arrived and the available pathways have become difficult to modify.
The Network Spine Must Be Commissioned as an External Interface
Inter-pod connectivity requires a defined network spine that supports the intended traffic flows and the physical connections between the individual computing units. The engineering team must identify where each pod hands off traffic, where spine equipment resides, how links reach their termination points, and how the wider fabric connects to the deployment. That architecture should specify link requirements, port assignments, routing arrangements, redundancy behavior, management access, and the procedures used to validate the complete connection path. Engineers should verify that the installed cable plant, switching equipment, optical components, and supporting power and cooling arrangements meet the approved network design for the deployment. This reconciliation should occur while the building’s cable pathways and equipment rooms remain accessible, not after the installation team has committed to a final arrangement.
Optical testing should verify the installed plant before the team connects it to the production fabric. Depending on the specified architecture, the acceptance process may include continuity checks, polarity verification, insertion-loss measurements, inspection of connector end faces, and other tests required by the optical design. The team should record test results against individual cable identifiers so that failures can be traced to a specific route or termination. Where the design requires redundant paths, engineers should validate each path independently and confirm that the intended redundancy behavior works across the relevant network components. Commissioning should also examine the complete connection from the pod handoff to the designated network destination rather than treating a successful cable test as proof of end-to-end functionality. Any temporary connection used during installation must be identified and replaced or formally accepted before operational release.
Site Environmental Envelope Assessment
A sealed factory-integrated system still operates within the physical environment that surrounds it, and that environment can affect reliability even when the internal assembly passes its factory tests. Ambient temperature, humidity, airborne contaminants, altitude, wind exposure, and seismic conditions influence equipment selection, installation methods, and the design of supporting infrastructure. Engineering teams must establish which environmental conditions apply to the exact installation location and compare them with the documented operating and storage limits of the delivered equipment. The assessment should cover both routine conditions and credible extremes that could affect operation, including seasonal temperature changes, wind-driven dust, moisture exposure, and interruptions to environmental control. Engineers should also distinguish the conditions encountered during transport and installation from those expected after the system enters service.
External Conditions Shape the Operating Boundary
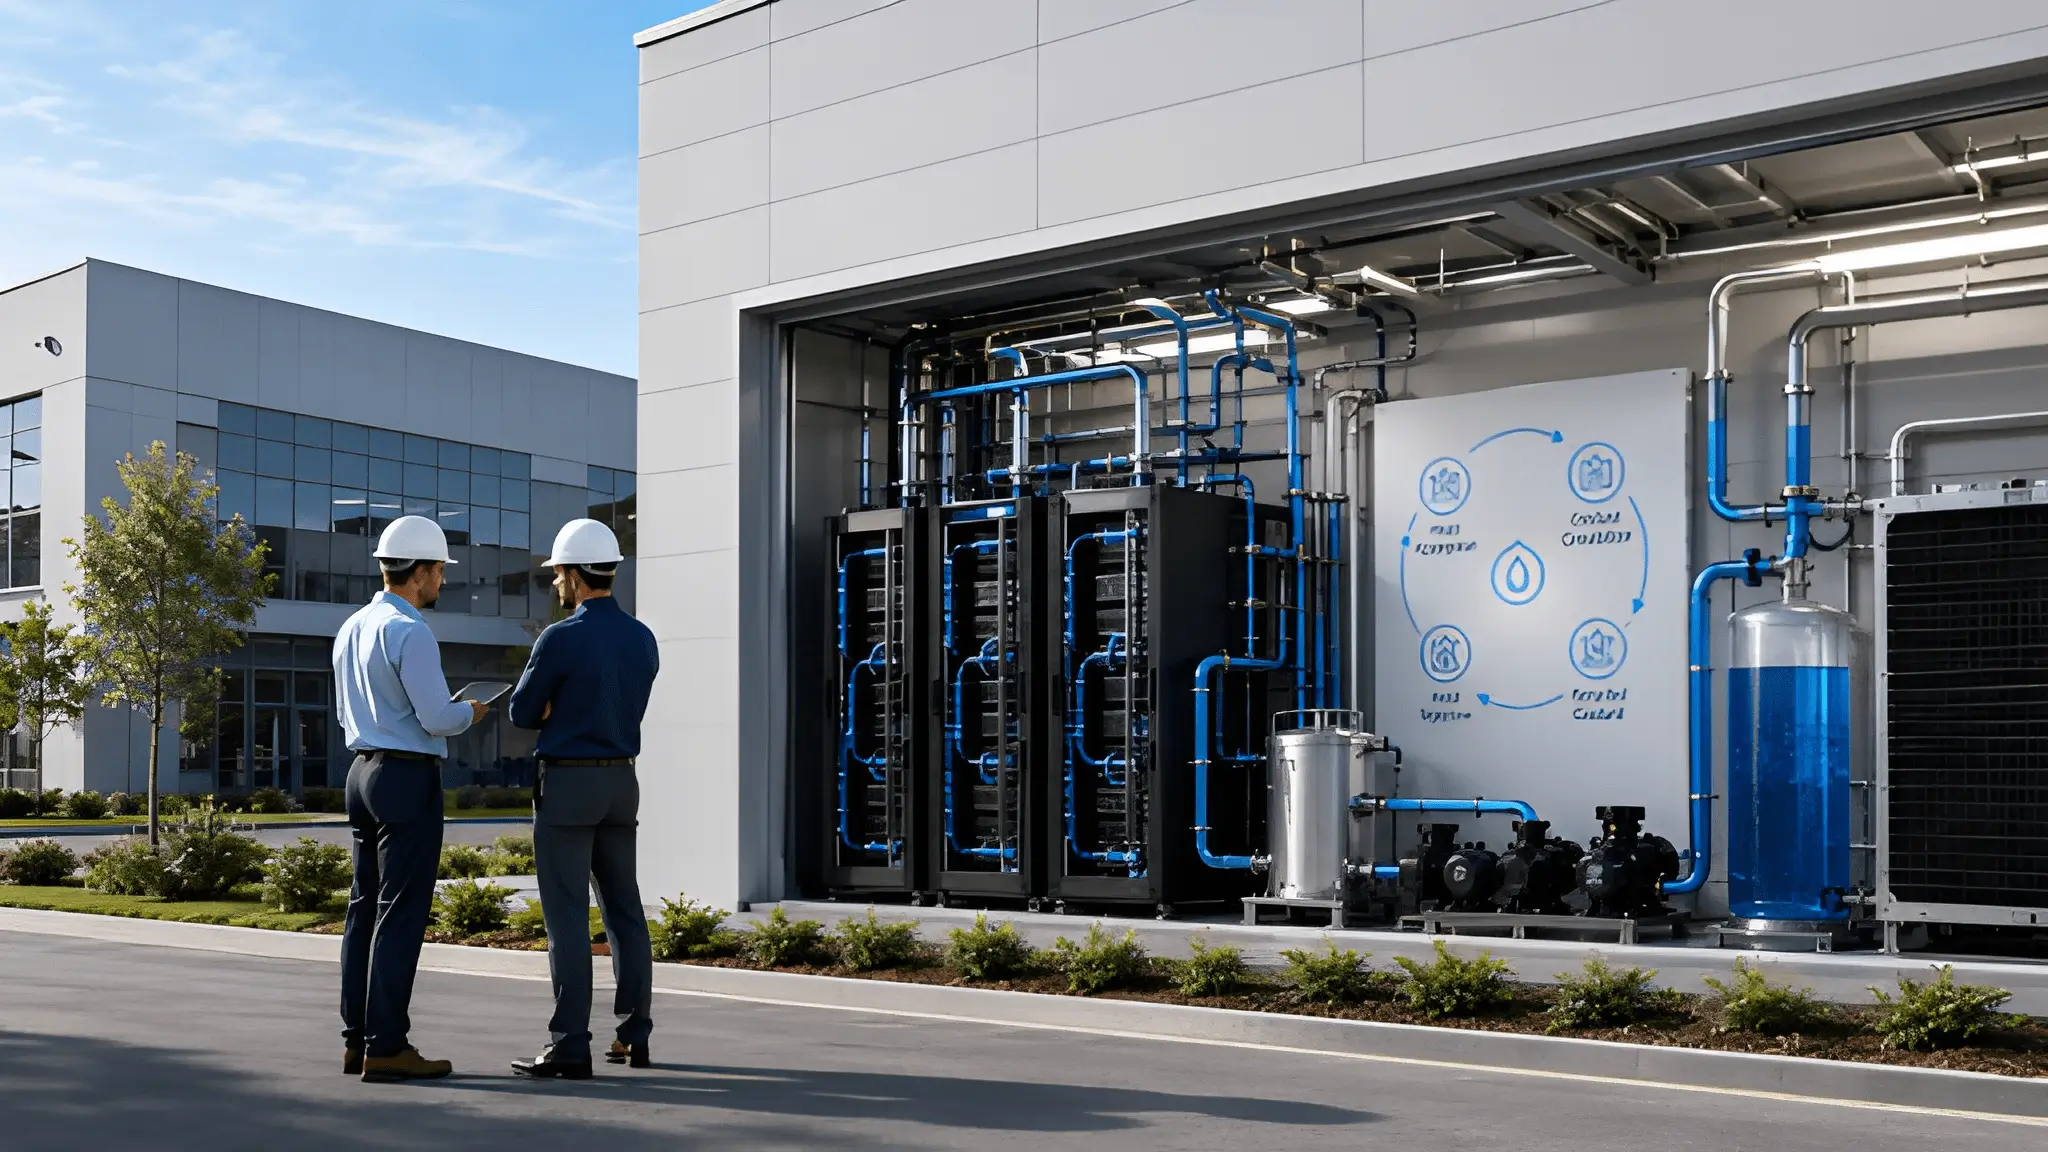
Ambient temperature affects the design of heat rejection, ventilation, equipment-room cooling, and any air-cooled components that support the installation. A cooling system sized around a favorable design condition may lose capacity when outdoor temperatures rise, while cold conditions can introduce freeze protection and fluid-management requirements. Engineers should assess the actual climate profile and the operating limits of chillers, dry coolers, pumps, heat exchangers, control systems, and other supporting equipment. The environmental assessment should evaluate heat recirculation, airflow restrictions, nearby exhaust sources, and intake and discharge locations wherever these conditions could affect equipment operation or the performance of the cooling system. These factors can create local conditions that differ from the weather data used during preliminary design.
Humidity and airborne contamination require assessment across both the equipment enclosure and the surrounding service environment. Moisture can affect exposed electrical connections, optical interfaces, stored components, and other materials when conditions fall outside their specified limits. Dust can obstruct filters, accumulate on equipment surfaces, interfere with airflow, and complicate maintenance, particularly when construction work continues near the installation. Engineers should identify nearby dust sources, construction traffic, industrial emissions, salt exposure, and other local conditions that could influence equipment protection requirements. Where the design calls for filtration, environmental monitoring, or controlled access, those measures must be installed and verified before the pod arrives. Teams should also establish how they will manage doors, service openings, and temporary barriers during delivery to avoid exposing protected equipment to uncontrolled conditions. Environmental acceptance should therefore consider the complete path from delivery through installation and operation, not merely the conditions measured inside the finished enclosure.
Altitude, Wind, Seismic Exposure, and Local Design Conditions
Altitude can influence equipment cooling and the performance of systems that depend on air density, making the installation location an important design input. Engineers should compare the site’s elevation with the documented operating limits of the selected equipment and verify whether any adjustments or additional design measures apply. The assessment should include supporting components because pumps, heat-rejection equipment, electrical systems, and control hardware may have different environmental limits from the computing equipment itself. Wind exposure also affects the design of external equipment supports, enclosures, screens, pipework, and other structures exposed to outdoor forces. The structural engineer must establish the applicable wind loads using the site’s location, exposure, geometry, and governing building requirements. A factory-integrated pod may arrive with a completed internal structure, but that does not automatically certify the foundations, anchorage, or surrounding equipment structures against local wind conditions.
Seismic assessment must consider the relationship between the pod, its support system, connected services, and the structure that carries the installation. Engineers should verify the applicable seismic design criteria and establish how the equipment will transfer forces through its anchors, base frames, restraints, and supporting structure. Piping and cable connections need suitable arrangements for the movement permitted by the approved design, without imposing damaging forces on equipment interfaces. The assessment should also address adjacent equipment and structures that could move differently during a seismic event. Where the site requires special anchorage, bracing, isolation, or flexible service connections, these measures must appear in the approved drawings and installation instructions. Contractors should not alter restraint locations or substitute connection hardware without the appropriate engineering review.
Sealed System Handling and Site Integrity Protocols
Factory integration moves critical assembly and validation work into a controlled environment, which changes the way teams must handle the equipment after dispatch. The receiving site should preserve the condition of the delivered system and avoid introducing damage or contamination during unloading, positioning, connection, and commissioning. Handling procedures must follow the actual equipment instructions, including restrictions on lifting, orientation, shock, vibration, storage, and the removal of shipping restraints. The site team should inspect the shipment for visible damage, packaging breaches, displaced components, and other signs that could require technical review before installation proceeds. Records should connect the shipping condition with the equipment’s identification and factory acceptance documentation, allowing the team to investigate any discrepancy.
Protecting Factory-Validated Equipment During Installation
A sealed enclosure should not be interpreted as permission to ignore the environmental conditions around the equipment or to open the system whenever an installation problem appears. Internal access may affect validated connections, contamination controls, warranty conditions, or the procedures required to restore the equipment to an approved state. If the team identifies a damaged interface, unexpected internal condition, or failed connection, it should record the issue and follow the designated technical escalation process. Unauthorized opening can complicate fault diagnosis by changing the equipment condition before the manufacturer or responsible engineering team has assessed the problem. The handling plan should therefore identify which tasks site personnel may perform, which actions require specialist authorization, and which issues require the equipment supplier’s involvement.
Delivery and installation procedures should establish controlled movement between transport, staging, final placement, and connection. The team should define who can enter the work area, who can direct lifting activities, and who can authorize changes to the approved installation sequence. Tools, lifting accessories, temporary covers, and connection materials should be inspected before use, particularly where they may contact sensitive interfaces or protected equipment surfaces. The site should also provide a suitable location for packaging removal and waste handling so that debris does not migrate into equipment openings or service connections. Contractors should avoid storing construction materials against the pod or using its enclosure as a support surface for unrelated work. A receiving inspection should record the external condition before and after placement, with photographs and written observations retained as part of the installation record.
Site Access, Contamination Control, and Configuration Integrity
Restricted access protects the equipment during the period when installation work, building activity, and external connections create competing demands on the receiving area. The site manager should establish access permissions, approved work zones, material movement routes, and responsibilities for maintaining environmental controls throughout the installation. Personnel entering the controlled area should understand the restrictions that apply to exposed interfaces, equipment openings, electrical connections, and cooling-system components. The procedures should also cover subcontractors whose work may generate dust, vibration, moisture, or debris near the installation. Where other construction activities continue nearby, physical barriers and work sequencing should prevent those activities from compromising the equipment’s protected condition.
The site integrity protocol should define how the team responds when inspection reveals damage, contamination, missing documentation, or an unexpected installation condition. Personnel should stop the affected activity when the issue could compromise safety, equipment integrity, or compliance with the approved procedure. The responsible engineer should document the condition, assess its significance, and determine whether specialist inspection, corrective work, additional testing, or formal approval is necessary. Teams should not close a deviation simply because the equipment appears operational, since some installation defects may remain undetected until the system experiences a particular operating condition. Corrective actions should include evidence that the identified problem has been resolved and that the affected interfaces meet their acceptance criteria. The final release should confirm that all required inspections, tests, configuration records, and authorized deviations have reached an acceptable status.
From Site Availability to Site Certification
The readiness of a site determines how effectively factory-integrated AI infrastructure can move from delivery into commissioning and operation. A completed building, available electrical connection, or cleared equipment area provides only part of the evidence needed to approve an installation. The complete assessment must establish that the access route supports the delivery configuration, the lifting area can accommodate the planned operation, and the structure can carry the installed equipment under its intended conditions. It must also confirm that electrical distribution, cooling capacity, heat rejection, network connectivity, and environmental controls match the requirements of the selected configuration. Each requirement depends on documented engineering evidence rather than assumptions carried forward from preliminary design.
Site Certification Becomes the Foundation of Deployment Velocity
The certification process should bring these requirements together in a controlled record that reflects the actual site and equipment configuration. Civil and structural approvals establish whether the delivery route, lifting positions, foundations, and support surfaces can accommodate the installation. Electrical and mechanical records demonstrate that the relevant utility interfaces, distribution arrangements, cooling circuits, and heat-rejection systems meet their approved requirements. Network acceptance confirms that the external fiber plant, termination points, and inter-pod connections support the intended computing architecture. Environmental and handling records establish that the equipment can reach its operating position without exposure to conditions that compromise its validated state. The commissioning team can then review these records against the acceptance plan and identify any unresolved dependency before approving delivery or installation.
Site certification also improves coordination because it gives each responsible party a defined set of deliverables and a clear basis for resolving outstanding work. Construction teams can close physical deficiencies before equipment arrives, while electrical, cooling, and network specialists can verify their interfaces against the approved configuration. Procurement and logistics teams can use the acceptance status to coordinate shipment without relying solely on projected construction dates. Commissioning personnel can identify which tests depend on completed external services and arrange their sequence around those dependencies. When a requirement remains unresolved, the project team can assign responsibility, document the corrective action, and establish the evidence needed for closure. This approach does not eliminate construction uncertainty, but it makes unresolved conditions visible before they disrupt the installation sequence. Site readiness consequently becomes a managed engineering deliverable rather than a broad description of construction progress.
Industrializing Readiness Without Treating Every Site as Identical
A repeatable certification process should establish consistent methods without imposing identical technical assumptions on every deployment. Sites differ in structural design, access constraints, climate, electrical architecture, cooling arrangements, network topology, and local regulatory requirements. The selected equipment configuration introduces another layer of variation because its weight, connection locations, support requirements, and environmental limits determine the conditions that the receiving site must satisfy. Engineering teams should therefore maintain a common readiness methodology while deriving acceptance criteria from the actual design, manufacturer documentation, and applicable codes. This arrangement allows operators to compare readiness across projects without overlooking local constraints or treating an earlier installation as automatic proof that another site will work.
The value of factory-integrated deployment ultimately depends on the quality of the interface between the completed product and the site that receives it. Internal integration can reduce the assembly work performed at the destination, but it cannot compensate for inadequate support structures, unsuitable environmental conditions, incomplete network pathways, or unavailable cooling capacity. Operators that establish clear certification criteria can identify those constraints while corrective work remains manageable and before delivery commitments create additional pressure. They can also coordinate transport, lifting, installation, and commissioning around verified conditions rather than broad declarations of construction progress. Vera Rubin site readiness is therefore not simply a condition of available space; it is a documented demonstration that the site can safely support, connect, and commission the intended infrastructure. That is the foundation on which factory-integrated deployment can deliver its intended advantage.